
In industrial filtration systems, removing water and contaminants from liquids and gases is essential for maintaining equipment performance, product quality, and operational efficiency. One of the most effective filtration arrangements involves using a coalescer followed by a separator filter element. While many engineers understand the role of a coalescer, there is often confusion about when a separator filter element should be installed after it and how it differs from a sintered filter cartridge.
Understanding the relationship between these filtration components can help industries optimize filtration performance, extend equipment life, and reduce maintenance costs. As a trusted filtration manufacturer, ZHUAN LV provides high-performance separator filter elements and sintered filter cartridges for a wide range of industrial applications.
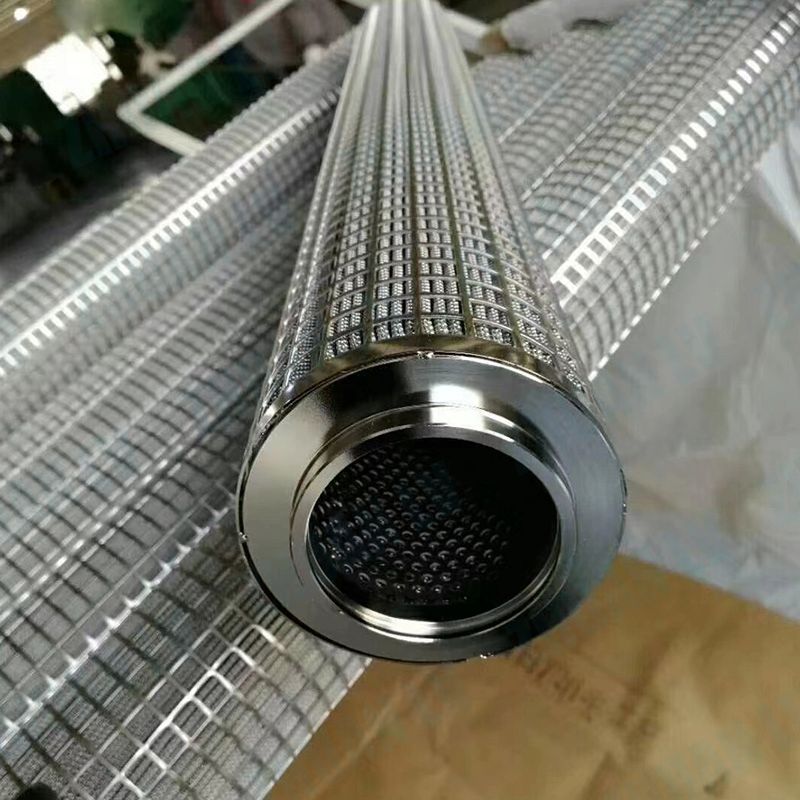
A coalescer and separator system is commonly used to remove water droplets, aerosols, and fine contaminants from liquids and gases.
The filtration process typically works in two stages:
1. Coalescing Stage – Small water droplets and aerosols are captured and merged into larger droplets.
2. Separation Stage – The separator filter element prevents the larger droplets from passing through and directs them away from the clean fluid stream.
This two-step process provides highly efficient water removal and is widely used in fuel filtration, natural gas processing, aviation fuel systems, and petrochemical operations.
A coalescer filter is designed to capture extremely fine liquid droplets suspended in a fluid stream. As the droplets pass through the coalescing media, they combine into larger droplets that become easier to remove.
However, the coalescer alone cannot always prevent these larger droplets from being carried downstream by fluid velocity.
A separator filter element acts as the second stage of protection. Its hydrophobic surface repels water and allows clean fuel or gas to pass through while preventing coalesced liquid droplets from re-entering the system.
Without a separator filter element, the efficiency of the coalescing process can be significantly reduced.
Aircraft fuel must meet extremely strict cleanliness and water-content requirements. Even small amounts of water can cause fuel contamination and operational risks.
In aviation filtration systems:
· The coalescer captures water droplets and particulates.
· The separator filter element removes the enlarged water droplets before fuel reaches the aircraft.
This combination ensures maximum fuel purity and system safety.
Natural gas streams often contain moisture and liquid aerosols that must be removed before transportation or processing.
A separator filter element is commonly installed after a coalescer to:
· Improve gas quality
· Protect compressors and turbines
· Prevent pipeline corrosion
· Reduce maintenance costs
Refineries use coalescer-separator systems to maintain product quality and protect sensitive processing equipment.
Applications include:
· Diesel filtration
· Jet fuel purification
· Chemical processing systems
· Hydrocarbon separation
If the fluid stream contains significant amounts of water, a separator filter element is highly recommended after the coalescer.
High moisture levels increase the likelihood that coalesced droplets will be carried downstream without proper separation.
Industries requiring ultra-clean fuels or fluids should use a separator filter element to maximize separation efficiency.
Examples include:
· Aviation
· Pharmaceutical manufacturing
· Semiconductor production
· Specialty chemical processing
Equipment such as turbines, pumps, compressors, and precision valves can be damaged by water contamination.
Installing a separator filter element provides an additional layer of protection.
A sintered filter cartridge is manufactured by compressing and heating metal powders into a porous filtration structure. These filters are known for their strength, durability, and high-temperature resistance.
They are commonly used for:
· Particle filtration
· Gas purification
· Catalyst recovery
· High-pressure applications
· Corrosive environments
Primary function:
· Water droplet separation
Advantages:
· Excellent liquid removal efficiency
· Hydrophobic surface treatment
· Designed for coalescer systems
Applications:
· Fuel filtration
· Gas dehydration
· Liquid-liquid separation
Primary function:
· Solid particle filtration
Advantages:
· High mechanical strength
· Reusable and cleanable
· High-temperature resistance
· Long service life
Applications:
· Industrial gas filtration
· Chemical processing
· Pharmaceutical manufacturing
· Hydraulic systems
While both components are filtration products, they serve different purposes and are often used in separate stages of industrial filtration systems.
A sintered filter cartridge is highly effective for removing solid particles but is generally not designed to perform the hydrophobic separation function of a separator filter element.
Using a sintered filter cartridge in place of a separator filter element may result in:
· Reduced water removal efficiency
· Higher moisture carryover
· Increased downstream contamination risks
Sintered filter cartridges are often installed:
· Upstream of coalescers
· In particulate removal stages
· In high-temperature filtration systems
· In applications requiring reusable filtration media
ZHUAN LV offers both separator filter elements and sintered filter cartridges to meet the specific requirements of different industrial processes.
Monitor filter condition and pressure drop to ensure optimal performance.
Damaged or saturated separator filter elements can reduce separation efficiency.
Select the correct separator filter element or sintered filter cartridge based on fluid type, contamination level, operating pressure, and temperature.
Proper installation and maintenance maximize filtration efficiency and equipment protection.
A separator filter element should be used after a coalescer whenever effective water removal is required from fuels, gases, or industrial fluids. While the coalescer combines small droplets into larger ones, the separator filter element prevents those droplets from re-entering the clean fluid stream, ensuring superior separation performance.
Although a sintered filter cartridge provides excellent particle filtration and durability, it serves a different purpose and cannot typically replace a separator filter element in coalescer-separator systems.
By selecting the right filtration solution, industries can improve product quality, protect critical equipment, and enhance operational efficiency. ZHUAN LV provides high-quality separator filter elements and sintered filter cartridges designed to deliver reliable performance across a wide range of demanding industrial applications.
Copyright:@2020-2021

Comments Please sign in or sign up to post.
0
0 of 500 characters used